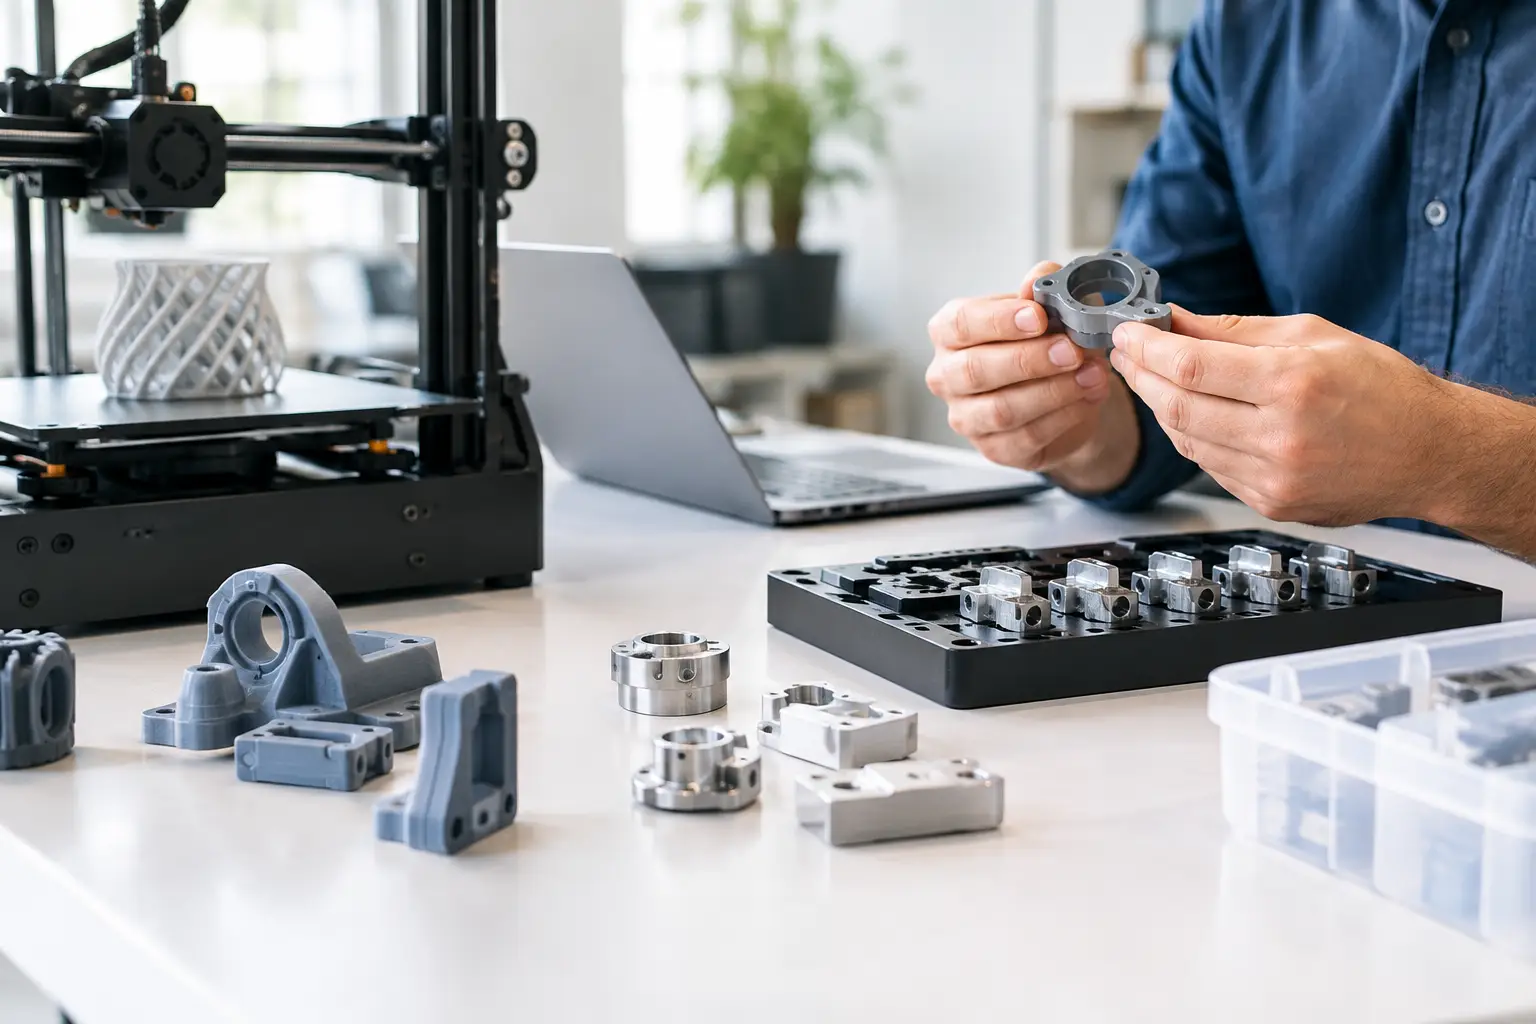
A promising prototype is not automatically ready for a 10,000-unit purchase order. Most new products need a practical middle stage: enough units to test demand, collect user feedback, support investor conversations, and refine the design without committing to expensive production tooling. That is where low volume manufacturing methods become a strategic advantage.
For inventors and founders, the right method is rarely the one with the lowest price per part on paper. The better question is whether it produces parts that accurately represent the product you intend to sell, at a quantity and timeline that support your next business decision. Materials, tolerances, finish, assembly requirements, intellectual property, and expected demand all affect the answer.
Why Low Volume Manufacturing Matters Before Scaling
Low-volume production generally covers anywhere from a few units to several thousand, depending on the product and process. It bridges the gap between one-off prototypes and full-scale manufacturing. Instead of spending heavily on hard tooling before the design is proven, you can build a controlled production run and learn from it.
That learning has real value. A limited run can reveal whether parts assemble consistently, whether a chosen material performs as expected, and whether packaging or shipping exposes weaknesses in the design. It can also help establish a credible cost model before you negotiate with high-volume suppliers.
For a patented or patent-pending invention, this stage deserves special care. Changes made for manufacturability may affect features that matter to the product’s function and protection strategy. Engineering, prototype development, and patent-focused planning should stay aligned rather than operating as separate projects.
The Main Low Volume Manufacturing Methods
Each method has a different strength. Some are ideal for functional engineering samples, while others make more sense when appearance, repeatability, or a small production run is the priority.
CNC Machining
CNC machining creates parts by removing material from a solid block of plastic, metal, or other machinable stock. It is one of the most dependable options when your product needs tight tolerances, durable materials, or precision mechanical features.
For example, a machined aluminum housing may be the right choice for a functional test of a handheld device, a fixture, or an industrial component. CNC also works well for low quantities because there is no mold to build. The trade-off is that complex shapes, deep internal features, and large quantities can become costly because each part requires machine time.
Machined parts may not always duplicate the economics of a future molded plastic part, but they can closely represent its fit, strength, and assembly needs when material selection is handled carefully.
3D Printing
3D printing is often the fastest path from a digital model to a physical part. It is valuable early in development because design changes can be made quickly, without reworking a mold or machining fixture. Technologies such as FDM, SLA, SLS, and metal printing each offer different surface finishes, material properties, tolerances, and cost structures.
This method is especially useful for concept models, ergonomic studies, enclosure iterations, jigs, fixtures, and limited functional runs. SLS nylon, for instance, can produce durable parts without support structures, while SLA can create detailed cosmetic models with a smoother surface.
The limitation is consistency with final production. Printed parts may have visible layer lines, anisotropic strength, or material behavior that differs from injection-molded plastic. That does not make 3D printing the wrong choice. It means the prototype must be evaluated for the question it is meant to answer. A part built to test button placement has different requirements than one built for a field durability trial.
Urethane Casting
Urethane casting uses a master pattern, often 3D printed or machined, to create a silicone mold. Liquid polyurethane is then poured into the mold to produce multiple copies. It is a strong option when you need more than a few parts with a molded appearance, detailed surfaces, or a range of colors and finishes.
For early product runs, urethane casting can deliver parts that look much closer to injection-molded components than many direct-printing methods. Silicone tooling is far less expensive and faster to produce than steel tooling, making it useful for market samples, pilot units, and pre-production evaluations.
However, silicone molds have a limited life, and part-to-part variation can increase as the mold ages. Casting is usually best for dozens or low hundreds of parts, not a long-term production plan. It is also important to design the master pattern with mold release, wall thickness, and undercuts in mind.
Sheet Metal Fabrication
Products with brackets, enclosures, panels, frames, or structural components may benefit from sheet metal fabrication. Laser cutting, bending, welding, and finishing can produce functional low-volume parts quickly, often in the same materials that will be used later in production.
This process is common for industrial equipment, electronics enclosures, appliances, and hardware products. It allows designers to make changes without investing in progressive stamping dies. A revised bend location or hole pattern is usually far easier to implement in a low-volume fabrication workflow than after production tooling has been ordered.
The main consideration is design discipline. Bend radii, flange dimensions, fastener access, weld distortion, and coating thickness all influence whether a part can be fabricated efficiently and assembled reliably.
Bridge Tooling and Injection Molding
Injection molding becomes more practical when demand is growing and the part must be made in production-grade plastic with repeatable quality. Bridge tooling, sometimes called soft tooling or prototype tooling, offers a middle path between temporary processes and high-volume hardened steel molds.
Aluminum or lower-life tooling can support limited production runs at a lower initial cost and shorter lead time than full production tooling. It is often appropriate for market launch quantities, regulatory samples, or early sales when the design is stable but demand has not yet justified a major tooling investment.
The trade-off is upfront cost. Even bridge tooling requires a serious commitment, and design changes can be expensive once the mold is cut. Before approving it, verify the part geometry, draft angles, wall thickness, material choice, shrink rate, cosmetic requirements, and expected production volume.
How to Choose the Right Method
The best manufacturing route starts with the decision you need the parts to support. If you are still proving the basic function, fast 3D-printed iterations may be the responsible choice. If you need to show a retailer, investor, or beta customer a product that looks and feels close to final, urethane casting, CNC machining, or a combination of processes may be more appropriate.
Ask four practical questions before selecting a process:
- What must these units prove: function, appearance, durability, assembly, market demand, or all of the above?
- How many units are needed before the next design decision or business milestone?
- Which features must match final production materials and which can be approximated for now?
- What design changes are still likely after testing?
A mixed approach is often the smartest answer. A product may use CNC-machined metal components for precision, printed internal features for fast iteration, and cast external housings for a more polished presentation. The goal is not to force every component into one manufacturing method. The goal is to produce reliable evidence that moves the product forward.
Design for Manufacturability Starts Early
Low-volume manufacturing should not be treated as a final handoff after design is complete. Manufacturing input during product development can prevent avoidable delays and redesigns. Small adjustments to wall thickness, fastener strategy, tolerances, snap features, surface finishes, and parting lines can materially change the cost and feasibility of a product.
This is particularly critical for electro-mechanical products. The enclosure, circuit board, battery, wiring, switches, heat management, and user-facing controls must work together. A beautiful housing that cannot be assembled efficiently or serviced safely is not ready for production.
At Industry of Concepts, product development is approached as a connected process: concept, engineering, prototype, manufacturability, and intellectual property considerations must support the same commercial objective. That coordination helps founders avoid building a prototype that impresses in a meeting but fails when it is time to produce consistent units.
Plan the Run Around Your Next Milestone
Do not order 500 parts simply because the unit cost looks better than ordering 50. If your design is likely to change after user testing, the extra inventory can become an expensive reminder of what you learned too late. Start with a quantity that provides meaningful feedback while preserving the flexibility to improve.
Conversely, do not stay in one-off prototype mode when the product is ready for real-world use. A disciplined low-volume run can give you better data on assembly time, quality control, supplier performance, packaging, and customer response. It turns assumptions into operating knowledge.
The right manufacturing method is the one that gives your idea a credible path forward without locking you into the wrong version of the product. Build the units that answer the next important question, then use what you learn to make the next decision with confidence.